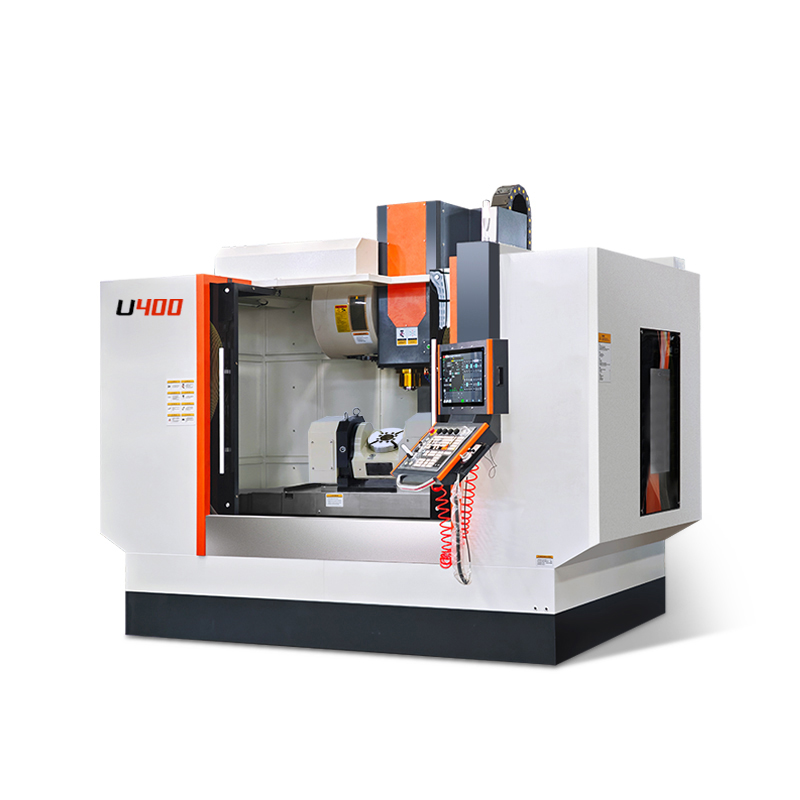
Most five-axis work that lands on a 400 mm table is not aircraft structure. It is valve bodies, hydraulic manifolds, small impellers, pump housings and shaft-type parts that need turning and milling in one clamping. The U400 is sized for that band of work: a 610 × 500 mm machining range on a machine still quick enough to make tool paths full of small moves worth running.
Three groups of numbers decide whether it fits a job: axis travels at 1300 / 700 / 750 mm on X / Y / Z; the table, a Ø400 mm dual direct-drive unit rated 200 kg with an Ø80H7 center hole and Ø60 mm through hole; and the spindle, an 11 kW direct-drive unit running to 12,000 rpm.
1300 mm of X Is About the Fixture, Not the Part
Buyers compare X travel against part length and stop there. That is the wrong comparison on a five-axis machine, because the table eats a large slice of the envelope. Put a Ø400 mm table on its trunnion, bolt a hydraulic fixture on top, and leave clearance for the tool to approach at an angle. By the time the setup is built, a machine with 900 mm of X has very little left over.
The U400 carries 1300 mm on X with 700 mm on Y and 750 mm on Z, enough to park the rotary assembly at one end of the stroke and still run a second operation. The 610 × 500 mm machining range is the honest figure for what can actually be cut once table geometry is accounted for, and it is the number to check against a drawing.
Y at 700 mm matters more than it looks. On a table-table five-axis machine, Y must cover the table diameter plus the swing of any fixture bolted to it, so a 400 mm table with a tall angle plate can eat most of a 500 mm stroke.
The Table: Dual Direct Drive, Ø400 mm, 200 kg
Both rotary axes are direct drive. There is no worm gear or preloaded gear set between motor and platter, which removes the two things that eventually degrade a geared table: backlash, and wear that has to be re-compensated every few months. The table holds its indexing over years instead of drifting by arc-minutes between service intervals.
The rated load is 200 kg, enough for a hydraulic fixture with four to six valve bodies, a small tombstone, or one heavy manifold with room for clamps. It is not a stack-of-castings table; that job belongs on a TMC630.
What the Ø80H7 Center Hole and Ø60 Through Hole Are For
The center hole is the detail that separates the U400 from the rest of the U series. Ø80H7 is a locating bore with an H7 fit, the tolerance class used when a fixture, adapter plate or chuck has to be centered to the table axis and stay there. Because it is a defined fit rather than a clearance hole, a mating spigot can be dialed in once and repeat after removal.
The Ø60 mm through hole is a passage from the table face down through the rotary assembly. Shops use it for three things. Bar stock passes through for shaft work that needs the end milled after turning. Hydraulic or pneumatic lines for a table-mounted fixture can be routed from below instead of looping across the work area. And coolant that would otherwise pool in a blind table drops straight through, taking most of the chips with it.
The smaller U320 has a Ø40 mm center hole; the U260 has Ø50 mm and an 80 kg load. If a job needs a large through bore, a heavy fixture, or both, the U400 is the only model in the U range that covers it.
Spindle: 11 kW, 12,000 rpm, No Gearbox in the Path
The spindle is a direct-drive mechanical unit rated 11 kW at 12,000 rpm maximum. Rotor and shaft are effectively one assembly, so there is no belt to stretch and no gear pair adding vibration at the top of the range. On aluminum that shows up as a better finish and a spindle that stays cooler through a long finishing pass.
Eleven kilowatts describes the machine’s intent honestly. It is comfortable in aluminum, brass, plastics and light cuts in mild steel, and it is not a heavy roughing spindle. Removing 5 mm per side from 4140 in one pass needs a BT50 box-way machine. The U400 rewards light depth of cut and high feed with small tools.
Where the U400 Sits in the U Series
The three U models share an architecture and differ almost entirely in scale. The U260 runs 850 / 600 / 600 mm with a Ø260 mm flange, Ø50 mm center hole and 80 kg load. The U320 steps to 1100 / 650 / 650 mm, Ø320 mm flange, Ø40 mm center hole and 150 kg. The U400 is the largest at 1300 / 700 / 750 mm, Ø400 mm flange, Ø80H7 center hole and 200 kg.
One detail in that comparison is easy to miss: the U320’s center hole is smaller than the U260’s, so the mid-size model is not simply a scaled-up small one. And the U400’s gain in X travel is proportionally larger than its gain in table diameter, which is what makes it usable for long parts as well as bulky ones.
U400 or LH400: Same Table Size, Different Layout
The LH400 also carries a Ø400 mm table rated 200 kg, with a BT40D spindle at 12,000 rpm, but its travels are 600 / 1000 / 600 mm on a 9,000 kg frame. The LH layout puts the long axis in Y; the U layout puts it in X.
That one difference decides jobs. Long narrow parts approached from the side as the table rotates favor the LH400’s 1000 mm of Y. Wide parts, or two setups side by side on one table, favor the U400’s 1300 mm of X.
Specifications
| Parameter | U400 |
|---|---|
| X / Y / Z axis travel | 1300 / 700 / 750 mm |
| Machining range | 610 × 500 mm |
| Rotary table | Dual direct drive |
| Mounting flange diameter | Ø400 mm |
| Center hole | Ø80H7 |
| Through hole | Ø60 mm |
| Max. table load | 200 kg |
| Spindle type | Direct-drive mechanical spindle |
| Max. spindle speed | 12,000 rpm |
| Spindle output power | 11 kW |
Practical Notes Before Ordering
Chip management should be settled at quotation, not after installation. With a through hole in the table, chips reach the lower area of the rotary assembly, and a conveyor sized for a three-axis VMC will not keep up. Specify it against material removal rate, not machine footprint.
If the machine will run unattended, say so early. A two-station tombstone only pays if the spindle runs through the night, which changes the through-spindle coolant, parts catcher and door interlock specification. All three are cheaper to add up front.
Asking for a Quote
Send the part drawing, material, fixture concept and batch size. BONANZA will confirm whether the U400 covers the envelope or whether the job belongs on a U320 or an LH400. Email sales@handemocnc.com or WhatsApp +86 173 0632 8370.
Related reading: the full 5-axis turning and milling machine range, the smaller U320, the compact U260, the LH400, and the larger TMC630.