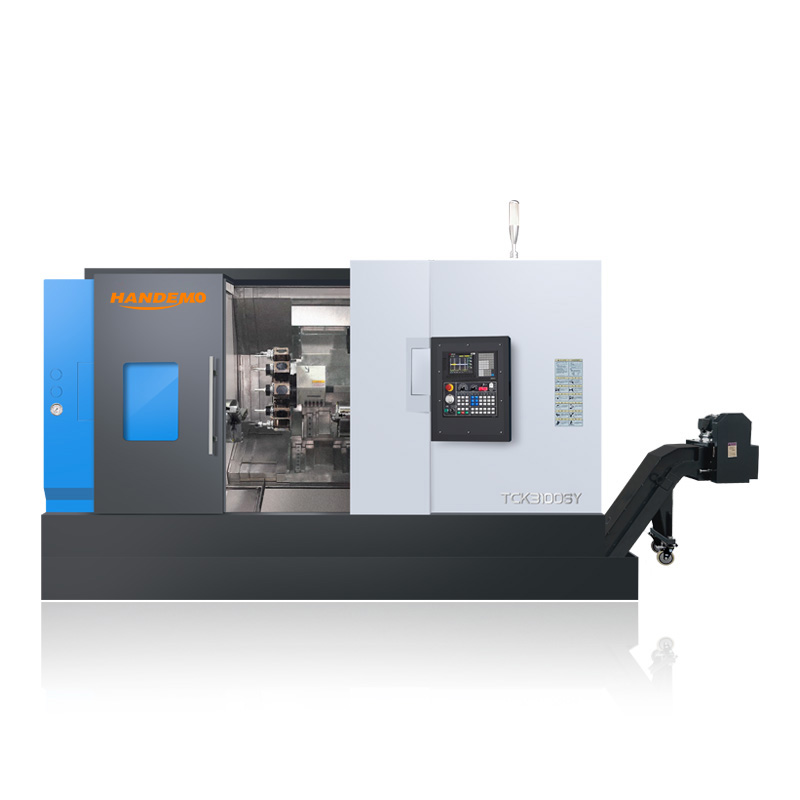
The 3100SY is the big one in BONANZA’s mill-turn line. It turns a part up to 500 mm across and 1,000 mm long, and it does the whole job on two spindles: an A2-8 main spindle with an 85 mm bore, and an A2-6 sub spindle on the back end that takes the part over for the second side without anyone opening a door.
At a glance: 750 mm of swing over the bed, an interpolated Y axis of plus or minus 100 mm, X travel of 400 mm and Z travel of 1,350 mm, a 12-station power turret, and 10,000 kg of casting under it all. Spindle motors are rated 37 kW on the main and 30 kW on the sub. The short version is that this is a machine for mid-size shafts, flanges, housings and gear blanks where the second operation costs more than the first.
3100SY at a glance
| Parameter | 3100SY |
|---|---|
| Max. swing over bed | 750 mm |
| Max. cutting diameter | 500 mm |
| Max. cutting length | 1,000 mm |
| Spindle nose type | A2-8 (main) / A2-6 (sub) |
| Main spindle bore diameter | 85 mm |
| Main spindle speed range | 3,000 rpm |
| Sub-spindle speed range | 4,000 rpm |
| Main spindle motor power | 37 kW |
| Sub-spindle motor power | 30 kW |
| X-axis travel | 400 mm |
| Z-axis travel | 1,350 mm |
| Y-axis travel (interpolated) | ±100 mm |
| Rapid traverse X / Y / Z | 12 / 12 / 16 m/min |
| Standard tool holder | 12-station power turret |
| Machine dimensions (L×W×H) | 4,450 × 2,320 × 2,713 mm |
| Machine weight | 10,000 kg |
Why the sub spindle matters more than the spec sheet suggests
Two things happen when you finish the back side on the same machine. You skip the second fixture, and you skip the re-datuming that comes with it. Concentricity between the two ends of a gear blank or a hub depends on how accurately the part was re-chucked, which means it depends on the operator and the fixture, not the machine. On the 3100SY the part moves from the A2-8 spindle to the A2-6 spindle mechanically, and every operation after that inherits the same centerline.
The two spindles are not the same size, and that is deliberate. The A2-8 side carries 85 mm through the bore at 3,000 rpm with a 37 kW motor, so the heavy roughing and the big diameter work happens there. The A2-6 sub spindle runs up to 4,000 rpm on a 30 kW motor, which suits the finish passes, the back facing, the small bores and the chamfering. A light sub spindle would waste the 37 kW roughing side, and a matched 37 kW sub would mean a bigger machine at a bigger price.
One clamping, six kinds of cutting
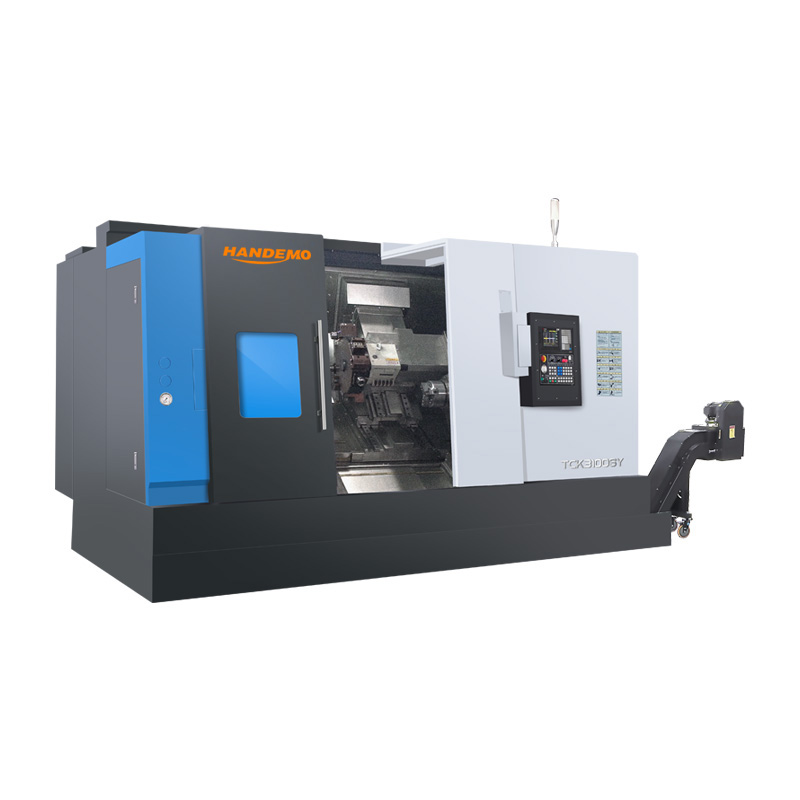
The 3100SY is listed as capable of turning, milling, planing, grinding, drilling and gear hobbing in a single clamping. The useful part is what it removes from the schedule: no queueing at the hobbing machine, no second op on the drill, no moving the part to a grinder after heat treat if the geometry allows grinding in place.
Gear hobbing on a mill-turn center is worth looking at closely if your parts are gear blanks. Hobbing normally needs its own machine and its own fixturing, and it is the step that most often gets sent out. Being able to hob the blank before it leaves the spindle keeps the gear teeth concentric with the bearing journal, which is where a lot of noise and wear complaints actually start.
If gear work is your driver, send the module, tooth count, face width and material with your inquiry. Hobbing capacity depends on the tooling package fitted, and BONANZA will confirm the working envelope for your part rather than quoting a generic figure.
The interpolated Y axis and what 100 mm buys
Y travel is plus or minus 100 mm, and because the Y axis interpolates, it can move in step with X, not just as a positioning axis. That means off-center drills, milled flats and slots, and contour milling at any angle, all on a lathe bed instead of in a second setup on a machining center.
A 12-station power turret sits on the machine and every station can drive a rotating tool. Twelve stations is usually more than the part needs, which is the point: a housing that needs a rough turn, a finish turn, a face groove, an internal thread, a milled pad, four drilled holes and a tapped hole can be tooled once and run through the cycle without stopping. The setup time disappears into the cycle time instead of sitting between operations.
The 2100LY shows the same idea at a smaller scale. Its turret mounts directly on the pallet, which drops the cutting center of gravity and lets it take 7 to 10 mm off one side in a single pass. The 3100SY carries the same layout in a heavier frame with a larger envelope and a second spindle.
Where the 3100SY sits in the mill-turn range
BONANZA builds several mill-turn platforms, and the differences are mostly about work envelope and how the part is held.
| Model | Max. cutting dia. | Max. cutting length | Spindle | Y axis |
|---|---|---|---|---|
| 3100SY | 500 mm | 1,000 mm | A2-8 main + A2-6 sub | ±100 mm, interpolated |
| TCK3100LY | 500 mm | 1,000 mm | A2-8, 85 mm bore | ±100 mm, interpolated |
| 2100LY | series dependent | series dependent | single spindle | interpolated |
| HTMC500T | 500 mm | 1,250 mm | A2-8, 86 mm bore | ±125 mm |
| HTMC800T | 600 mm | 1,500 mm | A2-6 / A2-8 | ±125 mm |
The TCK3100LY shares the 500 mm cutting diameter, the 1,000 mm cutting length and the 100 mm Y travel, so if your parts fit both, the deciding factors are the second spindle and the workholding arrangement rather than the envelope. The HTMC500T runs a longer cutting length at 1,250 mm and a wider Y axis at 125 mm, and it is built around a 14,000 kg frame. The HTMC800T steps up again to 600 mm cutting diameter, 1,500 mm cutting length and 17 tonnes of machine.
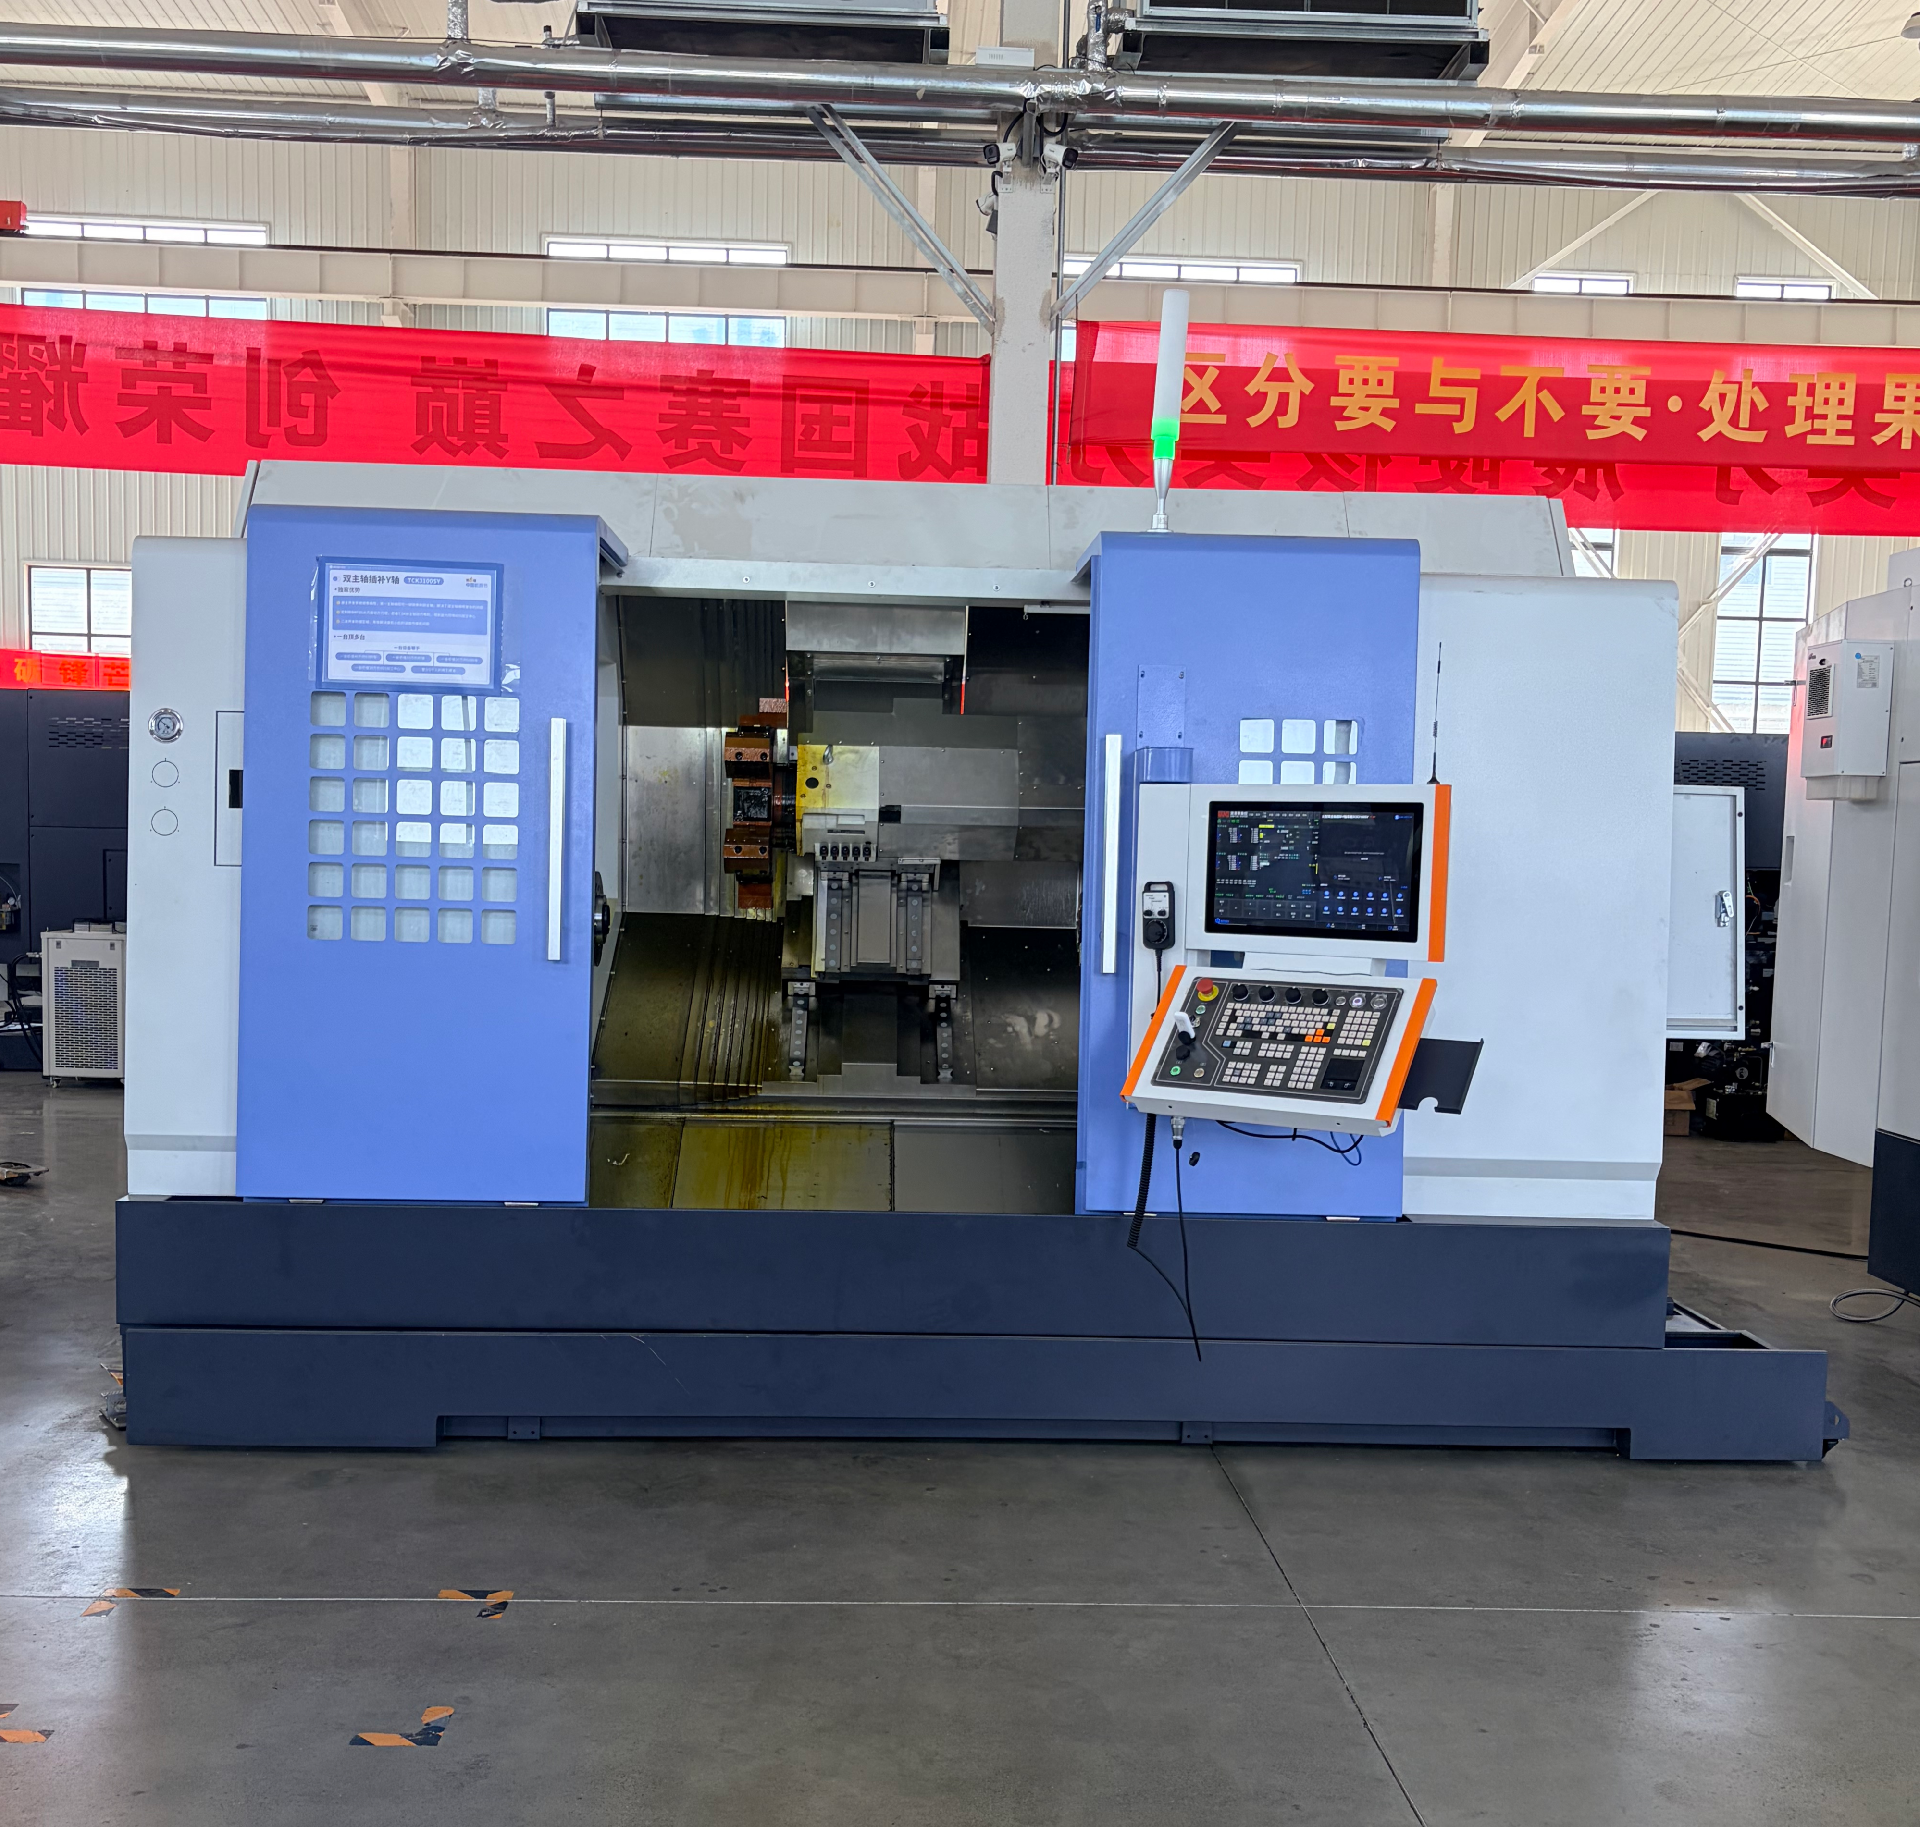
The 3100SY is the option when the part needs two sides machined in one setup and 500 mm by 1,000 mm covers the geometry. Below that, the work goes to the smaller machines; above it, the frame and turret grow with the HTMC series.
Footprint, weight and floor planning
The machine measures 4,450 mm long, 2,320 mm wide and 2,713 mm high, at roughly 10,000 kg. A 10,000 kg machine needs a floor that will take it and access for the lifting gear that puts it there. The Z axis runs 1,350 mm of travel against a 1,000 mm cutting length, which leaves room for the 12-station turret to approach and for the sub spindle to pick up the part without running out of stroke. Rapid traverse is 12 m/min on X and Y, 16 m/min on Z.
Questions buyers ask about the 3100SY
Can the 3100SY cut gears?
Yes, gear hobbing is listed as one of the operations the machine completes in a single clamping. The working range depends on the hobbing tool package and the blank diameter, so confirm the module and face width with the factory for your specific gear.
What is the bar capacity?
BONANZA publishes an 85 mm main spindle bore and an A2-8 nose. The maximum bar capacity that the chuck and the sub spindle will pass is not published on the specification sheet, so ask for it against your bar stock size before ordering.
How much floor space and power does it need?
The footprint is 4,450 by 2,320 mm. Total connected power and the supply configuration depend on the final spindle, tooling and control package, so request them with your quote.
Can it run unattended?
With a bar feeder on the main spindle and a part catcher at the sub spindle, the machine can run lights-out. Whether that pays off depends on cycle time and batch size, and BONANZA can quote the automation along with the machine.
Next step
If you are turning 500 mm parts in two or more operations, the 3100SY is worth pricing against your current process. Send a drawing or a part description with the material, the annual volume and the operations you run today, and BONANZA will come back with the machine configuration, the tooling list and a quote. Request a quote or message us on WhatsApp. More mill-turn platforms are listed under CNC Mill-Turn Machines.