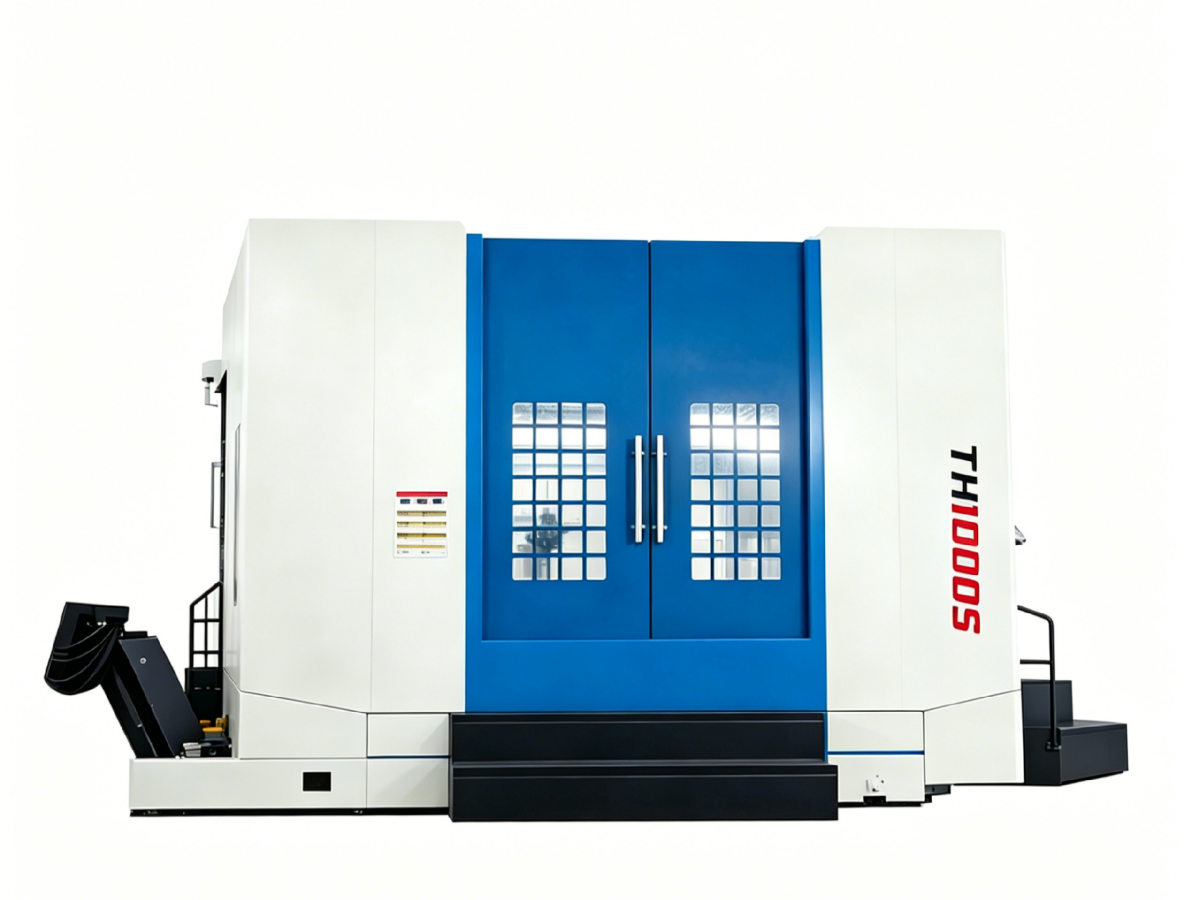
TH1000S Horizontal Machining Center – 4,000 kg Pallet with a 45° BT50 Spindle | BONANZA CNC
Most 1,000 mm pallet machines in the BONANZA range run a 6,000 rpm BT50-190 spindle. The TH1000S takes the other road. It pairs the same 1,000 x 1,000 mm pallet with a 45° BT50 spindle rated at 3,000 rpm, and carries 4,000 kg on the table instead of 3,500 kg. That swap is the whole argument for the machine, and it decides who should buy it.
Published figures: 1,000 x 1,000 mm table, 4,000 kg load, T-slots at 7-22-125 mm, travels of 1,800 / 1,000 / 1,300 mm on X / Y / Z, rapids of 14 / 12 / 14 m/min, BT50-45° spindle at 3,000 rpm, machine weight 16,000 kg. What those numbers mean in a shop is below.
A 1,800 mm X stroke on a square metre of pallet
The X stroke is 1,800 mm against a 1,000 mm pallet, so the table runs 400 mm past centre at each end. On a horizontal that margin is what lets you machine both end faces of a long housing, or reach the flange faces of a valve body, without unclamping and re-setting the part. On a 1,300 mm X machine working the same pallet you are down to 150 mm of overhang per side, and some parts will need a second operation just to get the last face.
Z at 1,300 mm is equally practical. A 1,000 mm pallet with a 1,300 mm Z stroke means a deep box can sit far enough forward to clear the column when the spindle is working the near face, and tools can reach into pockets that a short Z machine cannot enter at all. Y at 1,000 mm matches the pallet width, so the full face is reachable before you need a right-angle head.
The 7-22-125 mm T-slot pattern uses the same spacing as the TH1400S, which matters more than it sounds. Fixture plates and tombstone bases designed for one will bolt onto the other, so a shop running both sizes does not need two sets of fixtures.
The 45° BT50 spindle, and when 3,000 rpm is the limit you want
A 45° BT50 spindle is a heavy-cutting spindle. The 45° refers to the angle of the spindle head casting, which puts the drive and bearing support behind the cutting edge in a way that suits interrupted cuts, deep boring and cast-surface cleanup. The trade-off is speed: 3,000 rpm is the ceiling.
Where that works: cast iron and steel housings, valve and pump bodies, mould bases, boring operations, large-diameter face milling, and any part where a 100 mm cutter runs at 200 to 400 rpm and the limiting factor is torque, not spindle speed. On a 3,000 rpm spindle with BT50 tooling you can still run a 50 mm carbide face mill at healthy surface speed, and a 20 mm end mill is comfortable. What you do not want is a job built around 8 or 10 mm tools at 8,000 rpm finishing passes, because the spindle will not get there.
That is the real split in this range. The HMC1000 uses a BT50-190 spindle at 6,000 rpm with a 3,500 kg pallet, and it is the machine for a shop whose parts are mixed: heavy roughing plus a lot of small-hole drilling and light finishing. The TH1000S gives up spindle speed to gain 500 kg of pallet capacity and the heavier head, and it is the better answer when nearly every job is a big casting and the cutting is done with large tools.
Published specification
| Item | TH1000S |
|---|---|
| Table size | 1,000 × 1,000 mm |
| Max. worktable load | 4,000 kg |
| T-slot (number × width × distance) | 7-22-125 mm |
| X-axis travel | 1,800 mm |
| Y-axis travel | 1,000 mm |
| Z-axis travel | 1,300 mm |
| X-axis rapid traverse | 14 m/min |
| Y-axis rapid traverse | 12 m/min |
| Z-axis rapid traverse | 14 m/min |
| Spindle taper | BT50, 45° |
| Spindle speed | 3,000 rpm |
| Machine weight | 16,000 kg |
How it compares with the rest of the horizontal range
Reading the range as a table is faster than reading six pages. The figures below are the published numbers for each model.
| Model | Pallet | Max. load | X / Y / Z travel | Rapids (X/Y/Z) | Spindle | Weight |
|---|---|---|---|---|---|---|
| 630-DT | 630 × 630 mm | 1,200 kg | 1,100 / 900 / 1,000 mm | 18 / 15 / 15 m/min | BT50φ190, 6,000 rpm | 12,000 kg |
| 800S-DT | 800 × 800 mm | 2,000 kg | 1,300 / 1,000 / 1,000 mm | 15 / 12 / 12 m/min | BT50-45° | 15,500 kg |
| HMC1000 | 1,000 × 1,000 mm | 3,500 kg | 1,300 / 1,100 / 1,200 mm | 15 / 12 / 15 m/min | BT50φ190, 6,000 rpm | 18,000 kg |
| TH1000S | 1,000 × 1,000 mm | 4,000 kg | 1,800 / 1,000 / 1,300 mm | 14 / 12 / 14 m/min | BT50-45°, 3,000 rpm | 16,000 kg |
| TH1400S | 1,400 × 1,400 mm | 5,000 kg | 1,800 / 1,300 / 1,500 mm | 14 / 12 / 14 m/min | BT50-45°, 2,000 rpm | 19,500 kg |
| TH1600S | 1,600 × 1,600 mm | 10,000 kg | 2,000 / 1,500 / 1,800 mm | 12 / 12 / 12 m/min | BT50-45°, 1,500 rpm | 24,000 kg |
Two things stand out. First, the TH1000S is the lightest 1,000 mm pallet machine in the range at 16,000 kg, yet it carries 500 kg more than the HMC1000 at 18,000 kg. Second, its X stroke of 1,800 mm equals the TH1400S, which is a 1,400 mm pallet machine weighing 3,500 kg more. If your parts are long but not tall, that combination is worth checking against a larger machine on price and floor space.
The horizontal machining center series page lists the full range, including the 800-DT, TH500 and the HMC630II-ZT.
What the published sheet does not cover
The TH1000S page gives table, travels, rapids, spindle taper, spindle speed and machine weight. It does not give spindle motor power or torque, pallet indexing arrangement, ATC capacity and tool sizes, positioning and repeatability figures, guideway type, control model or the standard and optional equipment list. It also does not state whether the machine is supplied with a single table or a pallet changer.
Two of those gaps matter when you are comparing quotes. Spindle power and torque decide whether the 45° head can actually take the depth of cut you have in mind. Tool capacity and maximum tool diameter decide whether the ATC can hold the boring bars a 1,300 mm Z stroke invites. Ask for both in writing on the quotation, along with the positioning accuracy and the test standard behind it.
The published figures for the TH1000S also match those of the 1000S-DT line for line: same pallet, load, travels, rapids, spindle and weight. The two are quoted separately, so confirm with the factory which configuration sits behind each name before you specify one.
Who the TH1000S suits
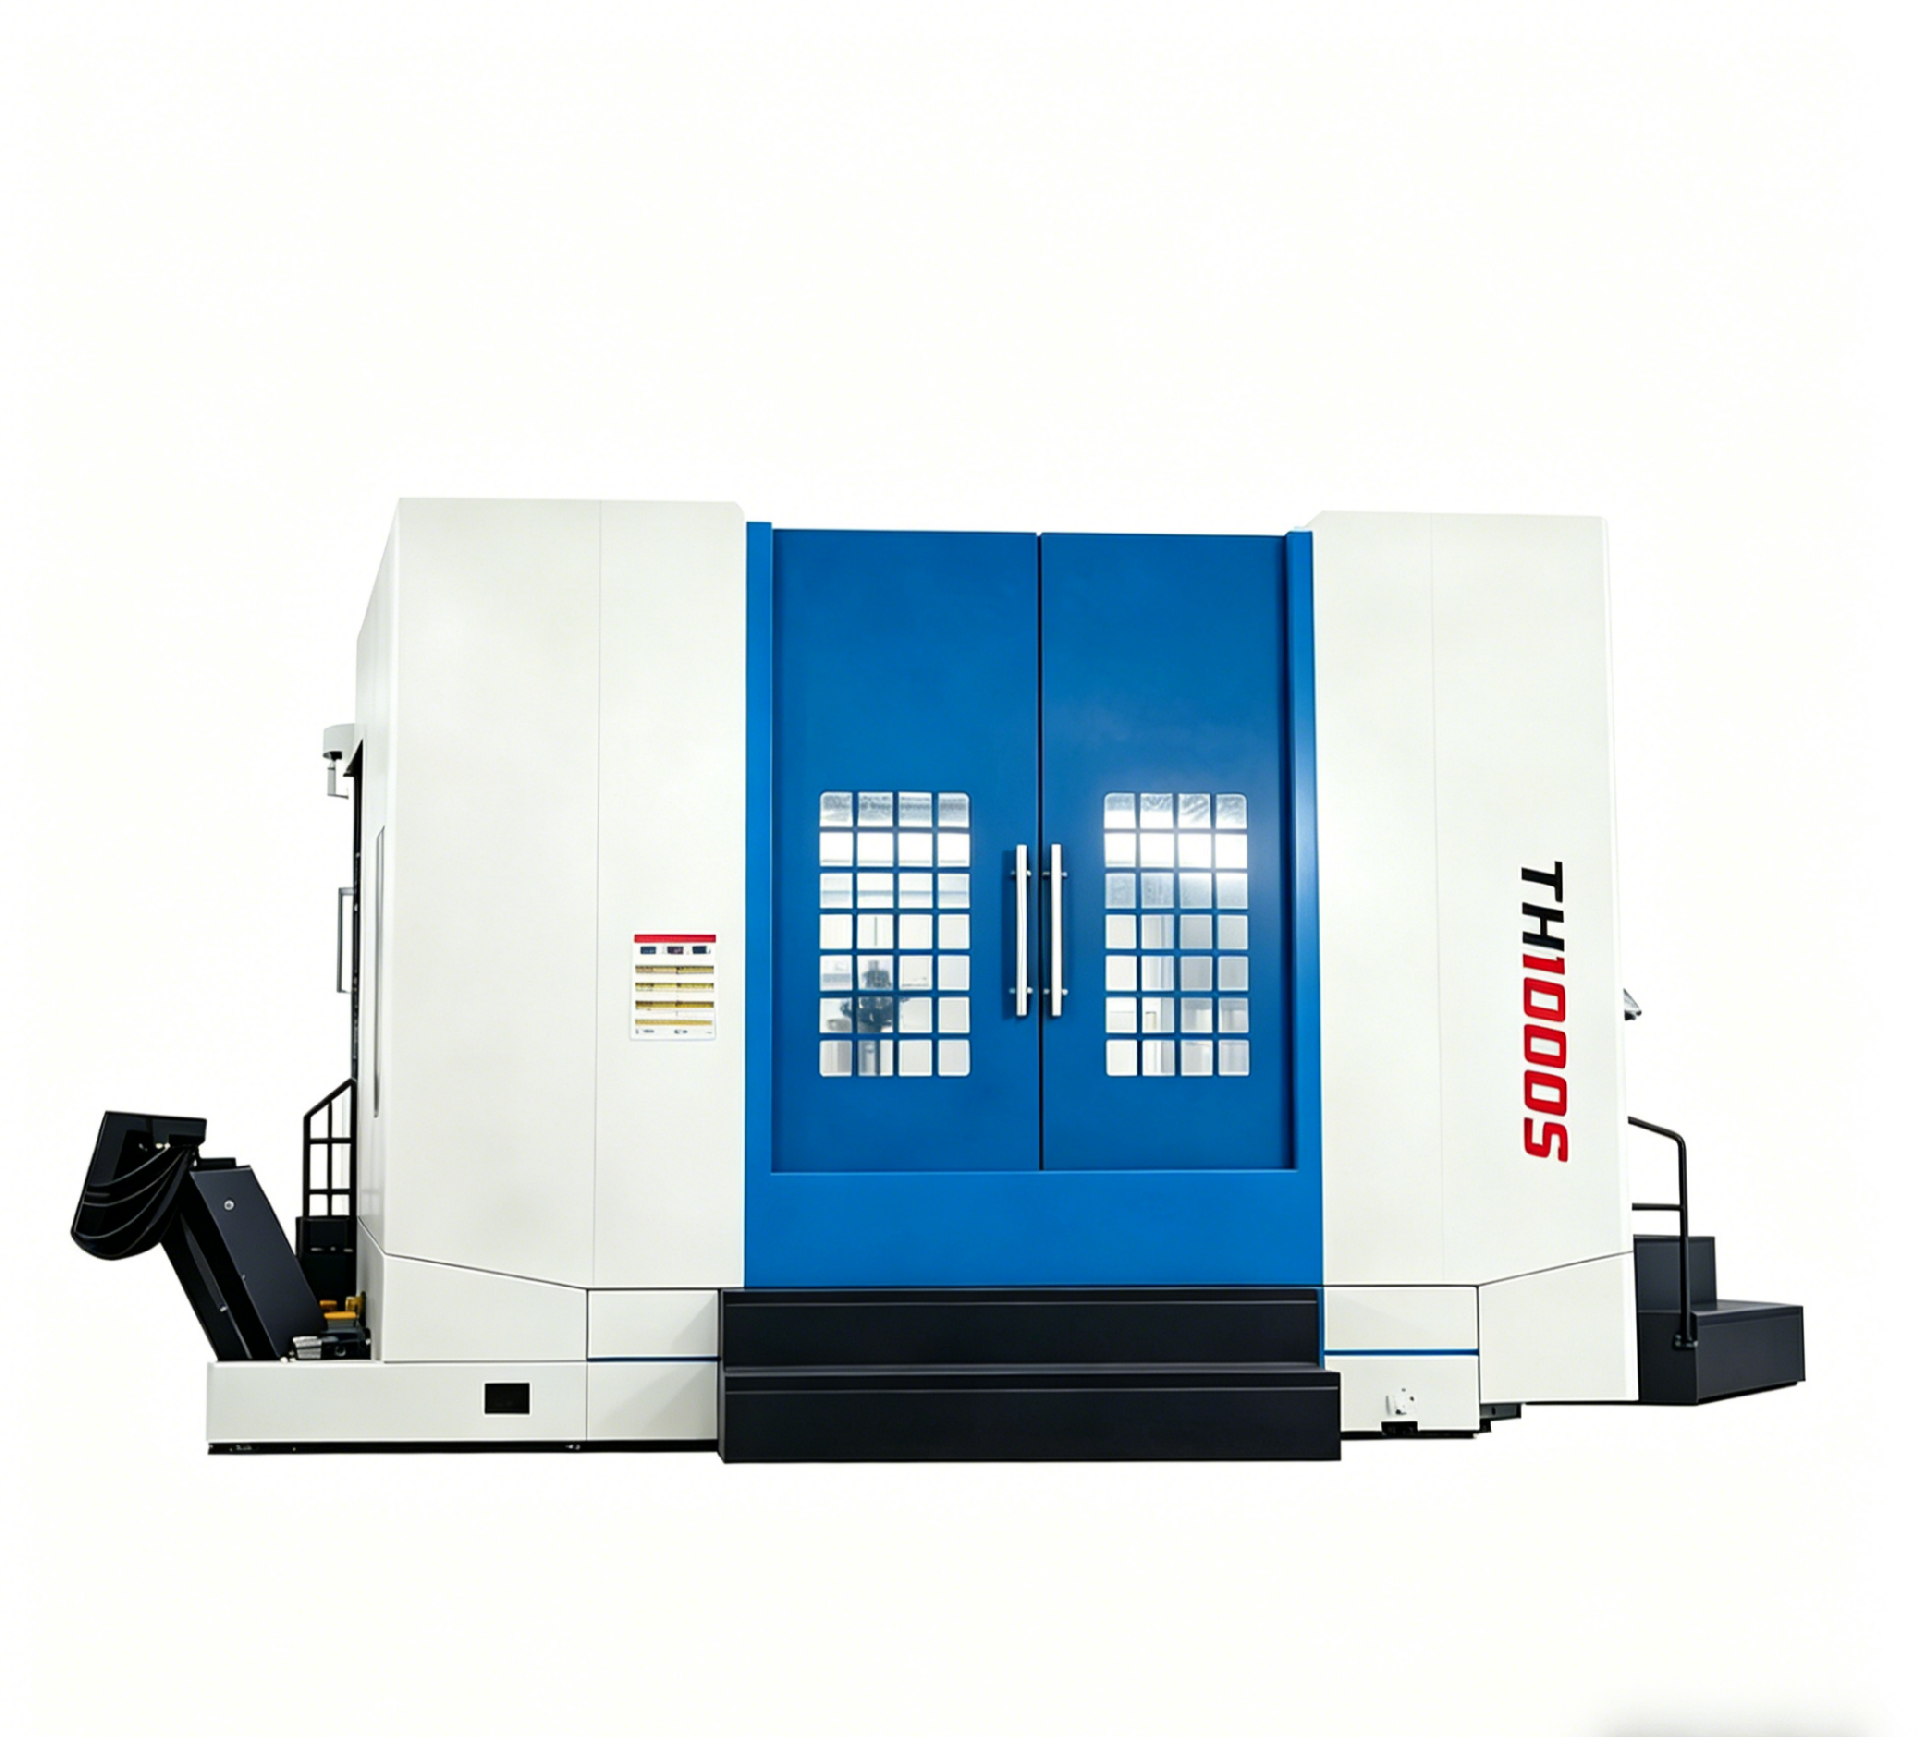
A shop machining large valve bodies, pump housings, gearbox castings and mould bases in low to medium volumes, where the part is heavy, the material removal is the bulk of the cycle, and the finishing is done with tools of 16 mm and up. Also a shop that has outgrown a 630 mm or 800 mm pallet machine on load capacity but does not have the floor space or the budget for a 1,400 mm machine, and whose parts are long enough that a 1,800 mm X stroke earns its keep.
It suits less well if the same machine has to drill hundreds of small holes per part at high speed. In that case the HMC1000 with its 6,000 rpm BT50-190 spindle will finish the light operations faster, and the 500 kg of lost capacity is usually recovered by running fixtures rather than solid blocks.
Bottom line
The TH1000S is a heavy-cutting 1,000 mm pallet machine, built around a 45° BT50 spindle at 3,000 rpm, 4,000 kg of table load and a 1,800 mm X stroke on a 16,000 kg frame. It is the machine in the range to look at when the parts are large castings, the tools are big, and spindle speed is not what limits the cycle.
Tell us the part size, weight and material and the operations you run, and we will confirm the spindle power, ATC configuration and accuracy figures for your quotation. Contact BONANZA for the TH1000S specification sheet and a price for the configuration you need.